| Size | Standard & Grade | Ends | Coating |
| OD: 406 - 1422.40mm, WT: 1.65 - 40mm, Length: 6mtr - 20mtr | ASTM A672 Grade A45, A55, B60, B65 etc. | Square Ends / Plain Ends (straight cut, saw cut, torch cut), Beveled / Threaded Ends | 3PE Coating; 3PP Coating; FBE Coating; Epoxy Coating; Special Painting |
American Piping Products stocks A672 EFW pipe in the grades and classes listed on the following tables:
| Plate specification | |||
| Pipe grade | Type of steel | ASTM specification | |
| No. | Grade | ||
| A 45 | plain carbon | A285 / A285M | A |
| A50 | plain carbon | A285 / A285M | B |
| A 55 | plain carbon | A285 / A285M | C |
| B 60 | plain carbon, killed | A515 / A515M | 60 |
| B 65 | plain carbon, killed | A515 / A515M | 65 |
| B 70 | plain carbon, killed | A515 / A515M | 70 |
| C 55 | plain carbon, killed, fine grain | A516 / A516M | 55 |
| C 60 | plain carbon, killed, fine grain | A516 / A516M | 60 |
| C 65 | plain carbon, killed, fine grain | A516 / A516M | 65 |
| C 70 | plain carbon, killed, fine grain | A516 / A516M | 70 |
| D 70 | manganese-silicon, normalized | A537 / A537M | 1 |
| D 80 | manganese-silicon, Q&TA | A537 / A537M | 2 |
| H 75 | manganese-molybdenum, normalized | A302 / A302M | A |
| H 80 | manganese-molybdenum, normalized | A302 / A302M | B, C or D |
| J 80 | manganese-molybdenum, Q&T | A533 / A533M | Cl-1B |
| J 90 | manganese-molybdenum, Q&T | A533 / A533M | Cl-2B |
| J 100 | manganese-molybdenum, Q&T | A533 / A533M | Cl-3B |
| K 75 | chromium-manganese-silicon | A202 / A202M | A |
| K 85 | chromium-manganese-silicon | A202 / A202M | B |
| L 65 | molybdenum | A204 / A204M | A |
| L 70 | molybdenum | A204 / A204M | B |
| L 75 | molybdenum | A204 / A204M | C |
| N 75 | manganese-silicon | A299 / A299M | |
| AQ&T = quenched and tempered BAny grade may be furnished |
| Class | Heat treatment of pipe | Radiography | Pressure test |
| 10 | none | no | no |
| 11 | none | yes | no |
| 12 | none | yes | yes |
| 13 | none | no | yes |
| 20 | stress relieved | no | no |
| 21 | stress relieved | yes | no |
| 22 | stress relieved | yes | yes |
| 23 | stress relieved | no | yes |
| 30 | normalized | no | no |
| 31 | normalized | yes | no |
| 32 | normalized | yes | yes |
| 33 | normalized | no | yes |
| 40 | normalized and tempered | no | no |
| 41 | normalized and tempered | yes | no |
| 42 | normalized and tempered | yes | yes |
| 43 | normalized and tempered | none | yes |
| 50 | quenched and tempered | none | none |
| 51 | quenched and tempered | yes | none |
| 52 | quenched and tempered | yes | yes |
| 53 | quenched and tempered | none | yes |
| Size | Standard & Grade | Ends | Coating |
| OD: 406 - 1422.40mm, WT: 1.65 - 40mm, Length: 6mtr - 20mtr | API 5L PSL1 / PSL2, GR.B, X42, X45, X50, X60, X65, X70, X80 | Square Ends / Plain Ends (straight cut, saw cut, torch cut), Beveled / Threaded Ends | 3PE Coating; 3PP Coating; FBE Coating; Epoxy Coating; Special Painting |
The steel for both seamless and welded pipe shall be made by one or more of the following processes: open-hearth, electric furnace, or basic-oxygen. The weld seam of electric-resistance welded pipe in Grade B shall be heat treated after welding.
| Chemical Requirements | Type S (seamless) |
Type E | Type F | ||
| Download Chart | (electric- resistance welded) |
(furnace- welded pipe) |
|||
| Grade A | Grade B | Grade A | Grade B | Grade A | |
| Carbon max. % | 0.25 | 0.30* | 0.25 | 0.30* | 0.3 |
| Manganese % | 0.95 | 1.2 | 0.95 | 1.2 | 1.2 |
| Phosphorous, max. % | 0.05 | 0.05 | 0.05 | 0.05 | 0.05 |
| Sulfur, max. % | 0 | 0.045 | 0.045 | 0.045 | 0.045 |
| Copper, max.% | 0.4 | 0.4 | 0.4 | 0.4 | 0.4 |
| Nickel, max. % | 0.4 | 0.4 | 0.4 | 0.4 | 0.4 |
| Chromium, max. % | 0.4 | 0.4 | 0.4 | 0.4 | 0.4 |
| Molybdenum, max. % | 0.15 | 0.15 | 0.15 | 0.15 | 0.15 |
| Vanadium, max. % | 0.08 | 0.08 | 0.08 | 0.08 | 0.08 |
| Standard Weight | |
| Single Random — 16′ – 22′. 5% may be jointers. If Plain Ends — 5% may be 12′ – 16′. | |
| Double Random — Shortest Length 22′, minimum average for order 35′. | |
| Extra Strong and Double Extra Strong | |
| Single Random — 12′ -22′. 5% may be 6′ – 12′. | |
| Double Random (XS and lighter) — Shortest Length 22′, minimum average for order 35′. | |
| Lengths longer than single random with wall thicknesses heavier than XS subject to negotiation. |
| Rolled, Stamped, or Stenciled (Mfrs. Option) |
| Name brand of manufacturer |
| Kind of pipe, that is, Continuous Welded, Electric-Resistance-Welded A, Electric-Resistance-Welded B, Seamless A, Seamless B, XS for extra strong, XXS for double extra strong. |
| ASTM 53 |
| Length of pipe |
| Couplings — Applied handling tight. Couplings, 2″ and smaller straight tapped, other sizes taper tapped. | |
| Thread Protection — Applied to pipe 4″ and larger. | |
| End Finish (unless otherwise specified) — | |
| STD or XS, or wall thicknesses less than 0.500 in. (excluding XXS): Plain and beveled | |
| All XXS and wall thicknesses over 0.500 in.: Plain end square cut. |
| Size | Standard & Grade | Ends | Coating |
| OD: 406 - 1422.40mm, WT: 1.65 - 40mm, Length: 6mtr - 20mtr | API 5L PSL1 / PSL2, GR.B, X42, X45, X50, X60, X65, X70, X80 | Square Ends / Plain Ends (straight cut, saw cut, torch cut), Beveled / Threaded Ends | 3PE Coating; 3PP Coating; FBE Coating; Epoxy Coating; Special Painting |
| Standard | Grade | Chemical Composition(%) | Tensile STrength(min) | Yield Strength(min) | |||
| C Mn P S | Mpa | Mpa | |||||
| API 5L PSL1 | A | 0.22 | 0.9 | 0.03 | 0.03 | 335 | 210 |
| B | 0 | 1.2 | 0.03 | 0.03 | 415 | 245 | |
| X42 | 0.28 | 1 | 0.03 | 0.03 | 415 | 290 | |
| X46 | 0.28 | 1.4 | 0.03 | 0.03 | 435 | 320 | |
| X52 | 0.28 | 1. 40 | 0.03 | 0.03 | 460 | 360 | |
| X56 | 0.28 | 1.4 | 0.03 | 0.03 | 490 | 390 | |
| X60 | 0.28 | 1.4 | 0.03 | 0.03 | 520 | 415 | |
| X65 | 0.28 | 1.4 | 0.03 | 0.03 | 535 | 450 | |
| X70 | 0.28 | 1.4 | 0.03 | 0.03 | 570 | 485 | |
| Standard | Grade | Chemical Composition(%) | Tensile STrength | Yield Strength | |||
| C Mn P S | Mpa | Mpa | |||||
| API 5L PSL2 | B | 0.24 | 1.2 | 0.025 | 0.015 | 415-655 | 245-450 |
| X42 | 0.24 | 1.3 | 0.025 | 0.015 | 415-655 | 290-495 | |
| X46 | 0.24 | 1.4 | 0.025 | 0.015 | 435-655 | 320-525 | |
| X52 | 0.24 | 1. 40 | 0.025 | 0.015 | 460-760 | 360-530 | |
| X56 | 0.24 | 1. 40 | 0.025 | 0.015 | 490-760 | 390-545 | |
| X60 | 0.24 | 1. 40 | 0.025 | 0.015 | 520-760 | 415-565 | |
| X65 | 0.24 | 1.4 | 0.025 | 0.015 | 535-760 | 450-600 | |
| X70 | 0.24 | 1.4 | 0.025 | 0.015 | 570-760 | 485-635 | |
| X80 | 0.24 | 1. 40 | 0.025 | 0.015 | 625-825 | 555-705 |
| PSL 1 | PSL 2 | ||
| Grade range | A25 through X70 | GR B through X80 | Table 1 |
| Size range | 0.405 through 80 | 4-2/1 through 80 | Table 1 |
| Type of pipe ends | Plain-end, threaded-end, bevelled-end, special coupling pipe | Plain-end | Table 1 |
| Seam welding | All methods continous welding limited to Grade A25 | All methods except continous and laser welding | Table 1 |
| Electric welds: welder frequency | No minimum | 100 kHz minimum | 5.1.3.3.2 |
| Heat treatments of electric welds | Required for grades > X42 | Required for all grades (GR B through X80) | 5.1.3.3.1; J.3.3.2:6.2.7 |
| Chemistry: max C for seamless pipe | 0.28% for grades > Gr B | 0.24% | Tables 2A, 2B |
| Chemistry: max C for welded pipe | 0.26% for grades > Gr B | 0.22% | Tables 2A, 2B |
| Chemistry: max P | 0.03% | 0.03% | Tables 2A, 2B |
| Chemistry: max S | Only when purchases specifies SR18 | 0.02% | Tables 2A, 2B |
| Carbon equivalent | None | Maximum required for each grade | 4.2:4.3:6.1.3: SR15.1 |
| Yield strength, maximum | None | Maximum for each grade | Tables 3A, 3B |
| UTS, maximum | None required | Maximum for each grade | Tables 3A, 3B |
| Fracture toughness | Only when purchaser specifies SR4 | Required for all grades | 6.2.6; 9.3.5: 9.8.4; 9.10.7; |
| Non-destructive inspection of seamless pipes | Permitted | SR4 mandatory | Table 14 9.7.2.6 |
| Repare by welding of pipe body, plate and skelp | Permitted by agreement | Prohibited | 5.3.2;9.7.6: B.1;B.2 |
| Certification | Certificates when specified per SR15 | Prohibited | 4.3;9.7.4.4;9.7.6;B.1.2;B.4 |
| Traceability | Traceable only until all tests are passed unless SR15 is specified | Certificates (SR15.1) mandatory Traceable after completion of tests (SR15.2) mandatory |
12.1 5.6 |
| Standard | Standard | |||||
| SY/T5040-2000 | Y/T5037-2000 | SY/T9711.1-197 | ASTM A252 | AWWA C200-9 | API 5L PSL1 | |
| Tube end OD deviation | ± 0.5%D | ± 0.5%D | -0.79mmรฏยฝลพ+2.38 | <± 0.1%T | <± 0.1%T | ± 1.6mm |
| Wall thickness | ± 10.0%T | D<508mm, ±12.5%T | - 8%Tรฏยฝลพ+19.5%T | <- 12.5%T | -8%Tรฏยฝลพ+19.5%T | 5.0mm |
| D>508mm, ±10.0%T | T≥15.0mm, ±1.5m |
| Size | Standard & Grade | Ends | Coating |
| OD: 406 - 1422.40mm, WT: 1.65 - 40mm, Length: 6mtr - 20mtr | API 5L PSL1 / PSL2, GR.B, X42, X45, X50, X60, X65, X70, X80 | Square Ends / Plain Ends (straight cut, saw cut, torch cut), Beveled / Threaded Ends | 3PE Coating; 3PP Coating; FBE Coating; Epoxy Coating; Special Painting |
| Standard | Grade | Chemical Composition(%) | Tensile STrength(min) | Yield Strength(min) | |||
| C Mn P S | Mpa | Mpa | |||||
| API 5L PSL1 | A | 0.22 | 0.90 | 0.030 | 0.030 | 335 | 210 |
| B | 0.28 | 1.20 | 0.030 | 0.030 | 415 | 245 | |
| X42 | 0.28 | 1.30 | 0.030 | 0.030 | 415 | 290 | |
| X46 | 0.28 | 1.40 | 0.030 | 0.030 | 435 | 320 | |
| X52 | 0.28 | 1. 40 | 0.030 | 0.030 | 460 | 360 | |
| X56 | 0.28 | 1.40 | 0.030 | 0.030 | 490 | 390 | |
| X60 | 0.28 | 1.40 | 0.030 | 0.030 | 520 | 415 | |
| X65 | 0.28 | 1.40 | 0.030 | 0.030 | 535 | 450 | |
| X70 | 0.28 | 1.40 | 0.030 | 0.030 | 570 | 485 | |
| Standard | Grade | Chemical Composition(%) | Tensile STrength | Yield Strength | |||
| C Mn P S | Mpa | Mpa | |||||
| API 5L PSL2 | B | 0.24 | 1.20 | 0.025 | 0.015 | 415-655 | 245-450 |
| X42 | 0.24 | 1.30 | 0.025 | 0.015 | 415-655 | 290-495 | |
| X46 | 0.24 | 1.40 | 0.025 | 0.015 | 435-655 | 320-525 | |
| X52 | 0.24 | 1. 40 | 0.025 | 0.015 | 460-760 | 360-530 | |
| X56 | 0.24 | 1. 40 | 0.025 | 0.015 | 490-760 | 390-545 | |
| X60 | 0.24 | 1. 40 | 0.025 | 0.015 | 520-760 | 415-565 | |
| X65 | 0.24 | 1.40 | 0.025 | 0.015 | 535-760 | 450-600 | |
| X70 | 0.24 | 1.40 | 0.025 | 0.015 | 570-760 | 485-635 | |
| X80 | 0.24 | 1. 40 | 0.025 | 0.015 | 625-825 | 555-705 |
| PSL 1 | PSL 2 | ||
| Grade range | A25 through X70 | GR B through X80 | Table 1 |
| Size range | 0.405 through 80 | 4-2/1 through 80 | Table 1 |
| Type of pipe ends | Plain-end, threaded-end, bevelled-end, special coupling pipe | Plain-end | Table 1 |
| Seam welding | All methods continous welding limited to Grade A25 | All methods except continous and laser welding | Table 1 |
| Electric welds: welder frequency | No minimum | 100 kHz minimum | 5.1.3.3.2 |
| Heat treatments of electric welds | Required for grades > X42 | Required for all grades (GR B through X80) | 5.1.3.3.1; J.3.3.2:6.2.7 |
| Chemistry: max C for seamless pipe | 0.28% for grades > Gr B | 0.24% | Tables 2A, 2B |
| Chemistry: max C for welded pipe | 0.26% for grades > Gr B | 0.22% | Tables 2A, 2B |
| Chemistry: max P | 0.03% | 0.03% | Tables 2A, 2B |
| Chemistry: max S | Only when purchases specifies SR18 | 0.02% | Tables 2A, 2B |
| Carbon equivalent | None | Maximum required for each grade | 4.2:4.3:6.1.3: SR15.1 |
| Yield strength, maximum | None | Maximum for each grade | Tables 3A, 3B |
| UTS, maximum | None required | Maximum for each grade | Tables 3A, 3B |
| Fracture toughness | Only when purchaser specifies SR4 | Required for all grades | 6.2.6; 9.3.5: 9.8.4; 9.10.7; |
| Non-destructive inspection of seamless pipes | Permitted | SR4 mandatory | Table 14 9.7.2.6 |
| Repare by welding of pipe body, plate and skelp | Permitted by agreement | Prohibited | 5.3.2;9.7.6: B.1;B.2 |
| Certification | Certificates when specified per SR15 | Prohibited | 4.3;9.7.4.4;9.7.6;B.1.2;B.4 |
| Traceability | Traceable only until all tests are passed unless SR15 is specified | Certificates (SR15.1) mandatory Traceable after completion of tests (SR15.2) mandatory |
12.1 5.6 |
| Standard | Standard | |||||
| SY/T5040-2000 | Y/T5037-2000 | SY/T9711.1-197 | ASTM A252 | AWWA C200-9 | API 5L PSL1 | |
| Tube end OD deviation | ± 0.5%D | ± 0.5%D | -0.79mmรฏยฝลพ+2.38 | <± 0.1%T | <± 0.1%T | ± 1.6mm |
| Wall thickness | ± 10.0%T | D<508mm, ±12.5%T | - 8%Tรฏยฝลพ+19.5%T | <- 12.5%T | -8%Tรฏยฝลพ+19.5%T | 5.0mm |
| D>508mm, ±10.0%T | T≥15.0mm, ±1.5m |
| Size | Standard & Grade | Ends | Coating |
| OD: 406 - 1422.40mm, WT: 1.65 - 40mm, Length: 6mtr - 20mtr | API 5L PSL1 / PSL2, GR.B, X42, X45, X50, X60, X65, X70, X80 | Square Ends / Plain Ends (straight cut, saw cut, torch cut), Beveled / Threaded Ends | 3PE Coating, 3PP Coating, FBE Coating, Epoxy Coating, Special Painting |
| Standard | Grade | Chemical Composition(%) | Tensile STrength(min) | Yield Strength(min) | ||||||
| c | Mn | P | S | Mpa | Mpa | |||||
| API 5L PSL1 | A | 0.22 | 0.90 | 0.030 | 0.030 | 335 | 210 | |||
| B | 0.28 | 1.20 | 0.030 | 0.030 | 415 | 245 | ||||
| X42 | 0.28 | 1.30 | 0.030 | 0.030 | 415 | 290 | ||||
| X46 | 0.28 | 1.40 | 0.030 | 0.030 | 435 | 320 | ||||
| X52 | 0.28 | 1. 40 | 0.030 | 0.030 | 460 | 360 | ||||
| X56 | 0.28 | 1.40 | 0.030 | 0.030 | 490 | 390 | ||||
| X60 | 0.28 | 1.40 | 0.030 | 0.030 | 520 | 415 | ||||
| X65 | 0.28 | 1.40 | 0.030 | 0.030 | 535 | 450 | ||||
| X70 | 0.28 | 1.40 | 0.030 | 0.030 | 570 | 485 |
| Standard | Standard | |||||
| SY/T5040-2000 | Y/T5037-2000 | SY/T9711.1-197 | ASTM A252 | AWWA C200-9 | API 5L PSL1 | |
| Tube end OD deviation | ± 0.5%D | ± 0.5%D | -0.79mmรฏยฝลพ+2.38 | <± 0.1%T | <± 0.1%T | ± 1.6mm |
| Wall thickness | ± 10.0%T | D<508mm, ±12.5%T | - 8%Tรฏยฝลพ+19.5%T | <- 12.5%T | -8%Tรฏยฝลพ+19.5%T | 5.0mm |
| D>508mm, ±10.0%T | T≥15.0mm, ±1.5m |
| Size | Standard & Grade | Ends | Coating |
| OD: 406-1422.40mm, WT: 1.65-40mm, Length: 6mtr - 20mtr | ASTM A250 Grades 1, 2, 3 | Square Ends/Plain Ends (straight cut, saw cut, torch cut), Beveled/Threaded Ends | 3PE Coating, 3PP Coating, FBE Coating, Epoxy Coating, Special Painting |
ASTM Specification A252 describes nominal (average) wall steel pipe piles of cylindrical shape and applies to pipe piles in which the steel cylinder acts as a permanent load-carrying member or as a shell to form case-in-place concrete piles.
Surface imperfections exceeding 25% of the nominal wall in depth are considered defects. Defects not exceeding 22.5% of the nominal wall in depth may be repaired by welding. Before welding, the defect shall be completely removed.
| Property | Grade 1 | Grade 2 | Grade 3 |
| Tensile Strength, min, psi | 50,000 | 60,000 | 66,000 |
| Yield Strength | 30,000 | 35,000 | 45,000 |
| - | Phosphorus |
| Seamless and Welded | Max% 0.050 |
| Specification | Size | Standard & Grade | Ends | Coating |
| Details | OD: 406-1422.40mm, WT: 1.65-40mm, Length: 6mtr-20mtr | ASTM A572 Grades 42, 50, 55, 60, 65 | Square Ends / Plain Ends (Straight Cut, Saw Cut, Torch Cut), Beveled / Threaded Ends | 3PE Coating, 3PP Coating, FBE Coating, Epoxy Coating, Special Painting |
| Type A | Element | Heat Analysis, % |
| 1 | Columbium | 0.005-0.05B |
| 2 | Vanadium | 0.01-0.15C |
| 3 | Columbium | 0.005-0.05B |
| 4 | Vanadium | 0.01-0.15C |
| 5 | Columbium plus Vanadium | 0.02-0.15D |
| 6 | Titanium | 0.006-0.04 |
| 7 | Nitrogen | 0.003-0.015 |
| 8 | Vanadium | 0.06 max |
A: Alloy content shall comply with Type 1, 2, 3, or 5 and shall be on test report.
B: Product analysis limits = 0.004 to 0.06%.
C: Product analysis limits = 0.005 to 0.17%.
D: Product analysis limits = 0.01 to 0.16%.
| Grade | Yield Point | Tensile Strength | Minimum Elongation (%) | |||
| min (ksi) | min (MPa) | min (ksi) | min (MPa) | "in 8 in (200 mm)" | "in 2 in (50 mm)" | |
| 42 [290] | 42 | [290] | 60 | [415] | 20 | 24 |
| 50 [345] | 50 | [345] | 65 | [450] | 18 | 21 |
| 55 [380] | 55 | [380] | 70 | [485] | 17 | 20 |
| 60 [415] | 60 | [415] | 75 | [520] | 16 | 18 |
| 65 [450] | 65 | [450] | 80 | [550] | 15 | 17 |
| Specification | Size | Standard & Grade | Ends | Coating |
| Details | OD: 406-1422.40mm, WT: 1.65-40mm, Length: 6mtr-20mtr | ASTM A671 Grade CA55, CB 60, CB 65, CB 70 etc. | Square Ends / Plain Ends (Straight Cut, Saw Cut, Torch Cut), Beveled / Threaded Ends | 3PE Coating, 3PP Coating, FBE Coating, Epoxy Coating, Special Painting |
| Pipe Grade | Steel Type | No. | Grade/Class/Type |
| CA 55 | Plain Carbon | A285/A285M | Gr C |
| CB 60 | Plain Carbon, Killed | A515/A515M | Gr 60 |
| CB 65 | Plain Carbon, Killed | A515/A515M | Gr 65 |
| CB 70 | Plain Carbon, Killed | A515/A515M | Gr 70 |
| CC 60 | Plain Carbon, Killed, Fine Grain | A516/A516M | Gr 60 |
| CC 65 | Plain Carbon, Killed, Fine Grain | A516/A516M | Gr 65 |
| CC 70 | Plain Carbon, Killed, Fine Grain | A516/A516M | Gr 70 |
| CD 70 | Manganese-Silicon, Normalized | A537/A537M | Cl 1 |
| CD 80 | Manganese-Silicon, Quenched and Tempered | A537/A537M | Cl 2 |
| CFA 65 | Nickel Steel | A203/A203M | Gr A |
| CFB 70 | Nickel Steel | A203/A203M | Gr B |
| CFD 65 | Nickel Steel | A203/A203M | Gr D |
| CFE 70 | Nickel Steel | A203/A203M | Gr E |
| CG 100 | 9% Nickel | A353/A353M | |
| CH 115 | 9% Nickel | A553/A553M | Type 1 |
| CJA 115 | Alloy Steel, Quenched and Tempered | A517/A517M | Gr A |
| CJB 115 | Alloy Steel, Quenched and Tempered | A517/A517M | Gr B |
| CJE 115 | Alloy Steel, Quenched and Tempered | A517/A517M | Gr E |
| CJF 115 | Alloy Steel, Quenched and Tempered | A517/A517M | Gr F |
| CJH 115 | Alloy Steel, Quenched and Tempered | A517/A517M | Gr H |
| CJP 115 | Alloy Steel, Quenched and Tempered | A517/A517M | Gr P |
| CK 75 | Carbon-Manganese-Silicon | A299/A299M | Gr A |
| CP 85 | Alloy Steel, Age Hardening, Quenched and Precipitation Heat Treated | A736/A736M | Gr A, Class 3 |
| Class | Heat Treatment on Pipe | Radiography, See Note | Pressure Test, See Note |
| 10 | None | None | None |
| 11 | None | 9 | None |
| 12 | None | 9 | 8.3 |
| 13 | None | None | 8.3 |
| 20 | Stress Relieved, See 5.3.1 | None | None |
| 21 | Stress Relieved, See 5.3.1 | 9 | None |
| 22 | Stress Relieved, See 5.3.1 | 9 | 8.3 |
| 23 | Stress Relieved, See 5.3.1 | None | 8.3 |
| 30 | Normalized, See 5.3.2 | None | None |
| 31 | Normalized, See 5.3.2 | 9 | None |
| 32 | Normalized, See 5.3.2 | 9 | 8.3 |
| 33 | Normalized, See 5.3.2 | None | 8.3 |
| 40 | Normalized and Tempered, See 5.3.3 | None | None |
| 41 | Normalized and Tempered, See 5.3.3 | 9 | None |
| 42 | Normalized and Tempered, See 5.3.3 | 9 | 8.3 |
| 43 | Normalized and Tempered, See 5.3.3 | None | 8.3 |
| 50 | Quenched and Tempered, See 5.3.4 | None | None |
| 51 | Quenched and Tempered, See 5.3.4 | 9 | None |
| 52 | Quenched and Tempered, See 5.3.4 | 9 | 8.3 |
| 53 | Quenched and Tempered, See 5.3.4 | None | 8.3 |
| 70 | Quenched and Precipitation Heat Treated | None | None |
| 71 | Quenched and Precipitation Heat Treated | 9 | None |
| 72 | Quenched and Precipitation Heat Treated | 9 | 8.3 |
| 73 | Quenched and Precipitation Heat Treated | None | 8.3 |
| Specification | Size | Standard & Grade | Ends | Coating |
| Details | OD: 406-1422.40mm, WT: 1.65-40mm, Length: 6mtr-20mtr | EN10219 Grade S235JRH, S275JOH, S275J2H, S355JOH, S355J2H, S355K2H | Square Ends / Plain Ends (Straight Cut, Saw Cut, Torch Cut), Beveled / Threaded Ends | 3PE Coating, 3PP Coating, FBE Coating, Epoxy Coating, Special Painting |
| Steel Grade | Steel Number | Type of De-oxidation | C (%) | Si (%) | Mn (%) | P (%) | S (%) | Nb (%) |
| S235JRH | 1.0039 | FF | 0.17 | — | 1.40 | 0.040 | 0.040 | 0.009 |
| S275J0H | 1.0149 | FF | 0.20 | — | 1.50 | 0.035 | 0.035 | 0.009 |
| S275J2H | 1.0138 | FF | 0.20 | — | 1.50 | 0.030 | 0.030 | — |
| S355J0H | 1.0547 | FF | 0.22 | 0.55 | 1.60 | 0.035 | 0.035 | 0.009 |
| S355J2H | 1.0576 | FF | 0.22 | 0.55 | 1.60 | 0.030 | 0.030 | — |
| S355K2H | 1.0512 | FF | 0.22 | 0.55 | 1.60 | 0.030 | 0.030 | — |
| Steel Grade | Steel Number | Minimum Yield Strength (ReH) MPa | Tensile Strength (Rm) MPa | Minimum Elongation (Ad) % | Minimum Impact Energy (KVe) J | Specified Thickness (mm) | Test Temperature |
| S235JRH | 1.0039 | 235 | 360-510 | 24 | 27 | £ 16 | -20°C |
| S275J0H | 1.0149 | 275 | 430-580 | 20 | 27 | £ 16 | -20°C |
| S275J2H | 1.0138 | — | — | 27 | — | — | - |
| S355J0H | 1.0547 | 355 | 510-680 | 20 | 27 | £ 16 | -20°C |
| S355J2H | 1.0576 | — | — | 27 | — | — | - |
| S355K2H | 1.0512 | 40 | — | — | — | — | - |
Steel Pipe Sourcing operates as a reputable steel industry company that delivers premium steel products for industrial purposes.
We offer a wide range of ASTM-compliant stainless steel pipes that are known for their exceptional strength, corrosion resistance, and longevity. Steel Pipe Sourcing is your trusted ASTM Stainless Steel Pipes in Mumbai.
Our branded pipes are known for their exceptional quality, reliable performance, and durability. Steel Pipe Sourcing offers a wide range of Branded Stainless Steel Pipes in Mumbai.
The numerous industries including construction and infrastructure alongside oil and gas transportation depend on steel pipes from Steel Pipe Sourcing as their fundamental structural element.
Our carbon steel tubes are widely used in various industries for structural, mechanical, and general engineering purposes. Steel Pipe Sourcing offers a comprehensive range of high-quality Carbon Steel Tube in Mumbai.
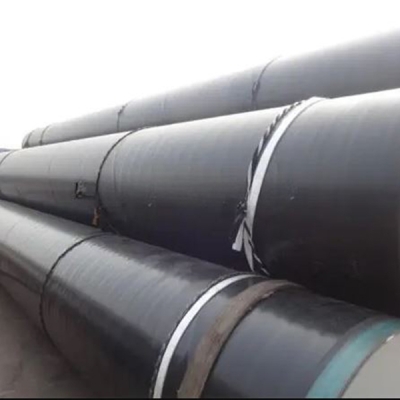
Steel Pipe Sourcing delivers premium welded carbon steel pipes for various industrial needs through standard and customized solutions.
At Steel Pipe Sourcing, we take immense pride in offering a comprehensive range of high-quality Casing and Tubing solutions that cater to diverse industrial needs. As a prominent name for Casing and Tubing in Mumbai.
Our duplex steel products exhibit exceptional strength and corrosion resistance, making them suitable for a wide range of industrial applications. Steel Pipe Sourcing is a trusted provider of Duplex Steel Plate Sheet coil in Mumbai.
Our Duplex Super Duplex pipes are manufactured using high-grade materials and advanced manufacturing techniques, ensuring reliable performance in demanding environments.
We offer a comprehensive range of high-quality Jindal stainless steel pipes that are manufactured using advanced technology and state-of-the-art machinery. Steel Pipe Sourcing is your trusted destination for Jindal Stainless Steel ERW Pipes in Mumbai.
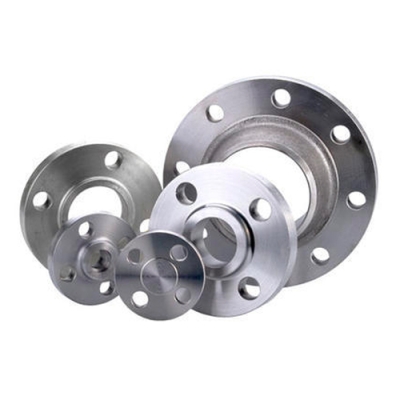
Our flanges are manufactured using high-quality materials and are available in different sizes, shapes, and specifications in Mumbai. Steel Pipe Sourcing is a well-known name among the Flanges in Mumbai.
Our extensive range includes pipes, tubes, fittings, and more, manufactured from these corrosion-resistant alloys. Steel Pipe Sourcing is your reliable Inconel Monel Hastelloy in Mumbai.
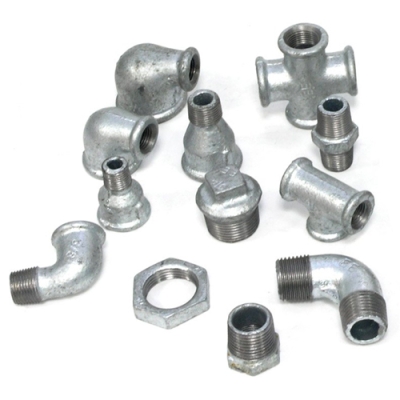
We offer a wide range of pipe fittings that are designed to meet diverse industrial requirements. Steel Pipe Sourcing is a trusted provider of high-quality Pipe Fittings in Mumbai.
We offer a wide range of seamless pipes and tubes that are manufactured using high-quality stainless steel. Steel Pipe Sourcing is a trusted provider of Seamless Stainless Steel Pipes Tubes in Mumbai.
Steel Pipe Sourcing operates as an established steel industry leader which provides top-quality pipes to serve various industrial needs.
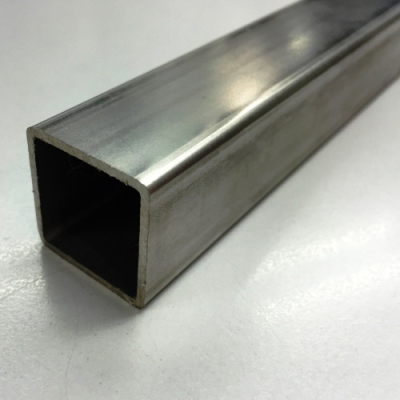
Our square pipes are made from high-quality materials and are known for their strength, durability, and dimensional accuracy. Steel Pipe Sourcing offers a Square Pipe in Mumbai.
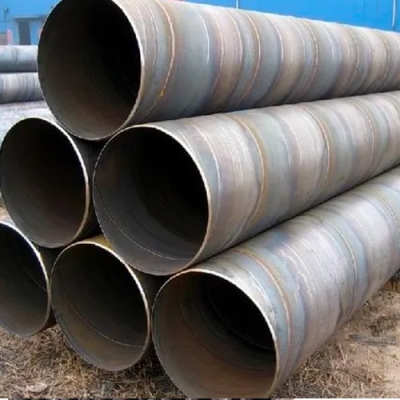
Our SSAW steel pipes are known for their strength, durability, and versatility in various industrial applications. Steel Pipe Sourcing offers a wide range of SSAW Steel Pipe in Mumbai.
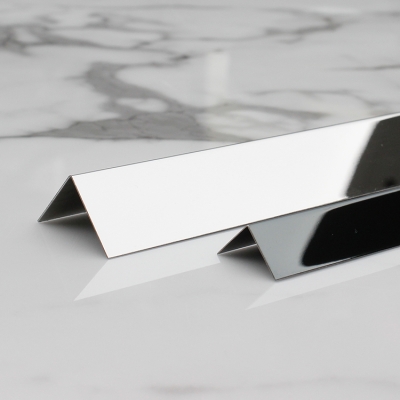
Our decorative profiles are designed to add a touch of elegance and sophistication to architectural and interior design projects. Steel Pipe Sourcing offers a wide range of Stainless Steel Decorative Profiles in Mumbai.
We offer a wide range of seamless pipes and tubes that are manufactured using high-quality stainless steel. Steel Pipe Sourcing is a trusted provider of Stainless Steel Pipes Tubes in Mumbai.
We offer a comprehensive range of stainless steel products that are suitable for various industrial applications. Steel Pipe Sourcing is your reliable source for Stainless Steel Plate Sheet Coil in Mumbai.
The steel products from Steel Pipe Sourcing serves multiple industries including construction and infrastructure and engineering.
Our welded stainless steel pipes are manufactured using advanced welding techniques and high-quality stainless steel material. Steel Pipe Sourcing offers a wide range of Welded Stainless Steel Pipe in Mumbai.